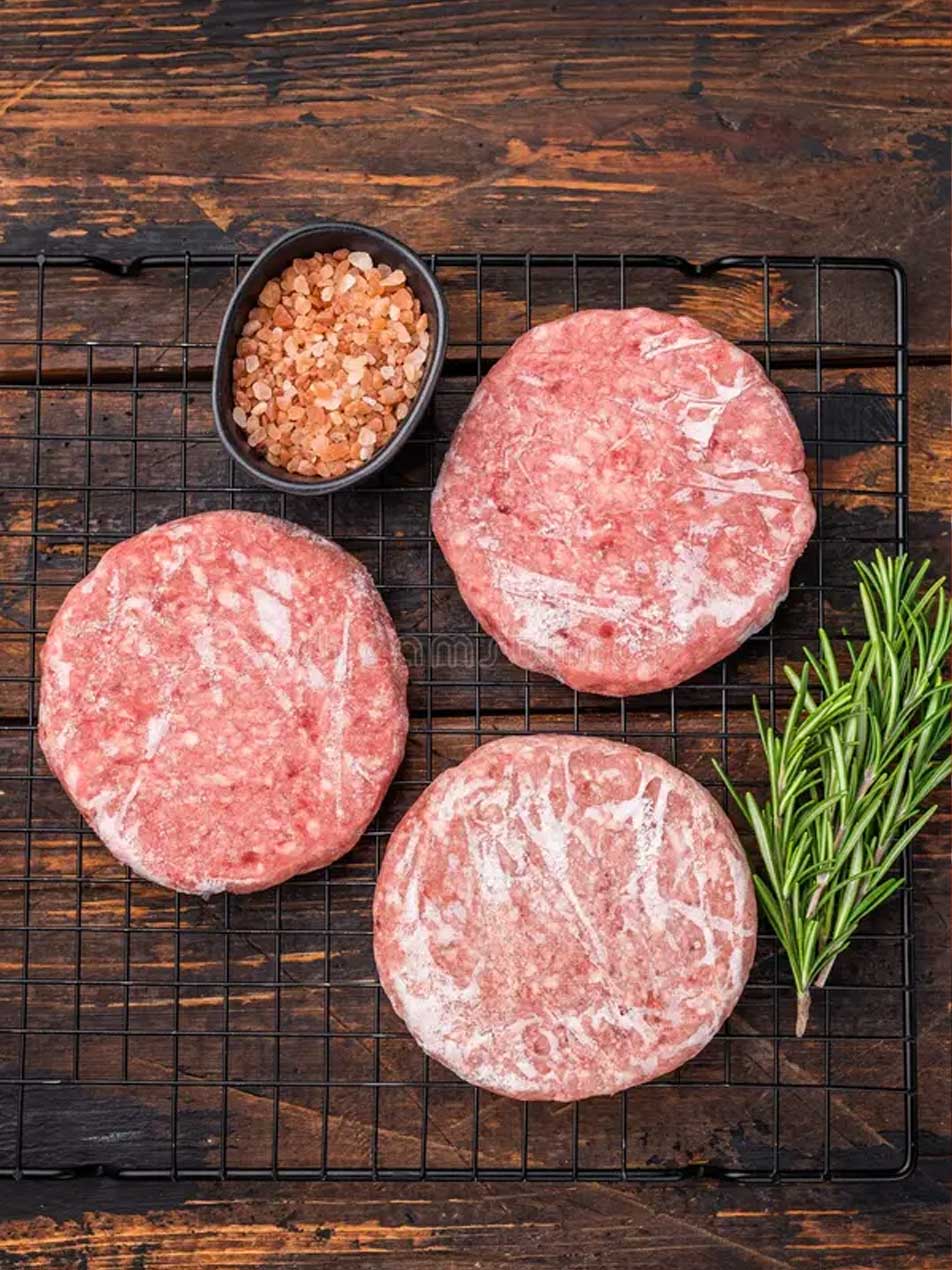
Packaged Meat & Poultry
Freezes 15 to 30 kg master cartons of boxed beef, pork, and poultry cuts to −18°C core temperature with flat, stackable box geometry.

Square’s automated carton freezer chills and freezes boxed beef, pork, poultry, seafood, and dairy in master cartons or plastic totes from 2 to 15 tons/h.
With automatic conveyor loading, multiple tiers, fast horizontal airflow, and barcode tracking, the system freezes mixed box sizes at once and replaces manual blast room handling.
Simultaneous multi SKU carton retention times
PLC/SCADA control with servo monitoring and remote diagnostics
Uniform horizontal crossflow airflow across all conveyor tiers
Automated infeed, tier loading, and discharge eliminate manual blast room handling
Full barcode batch and dwell time traceability integrated with plant WMS

Product Features
Automated box handling, horizontal airflow, and barcode tracking for boxed foods.
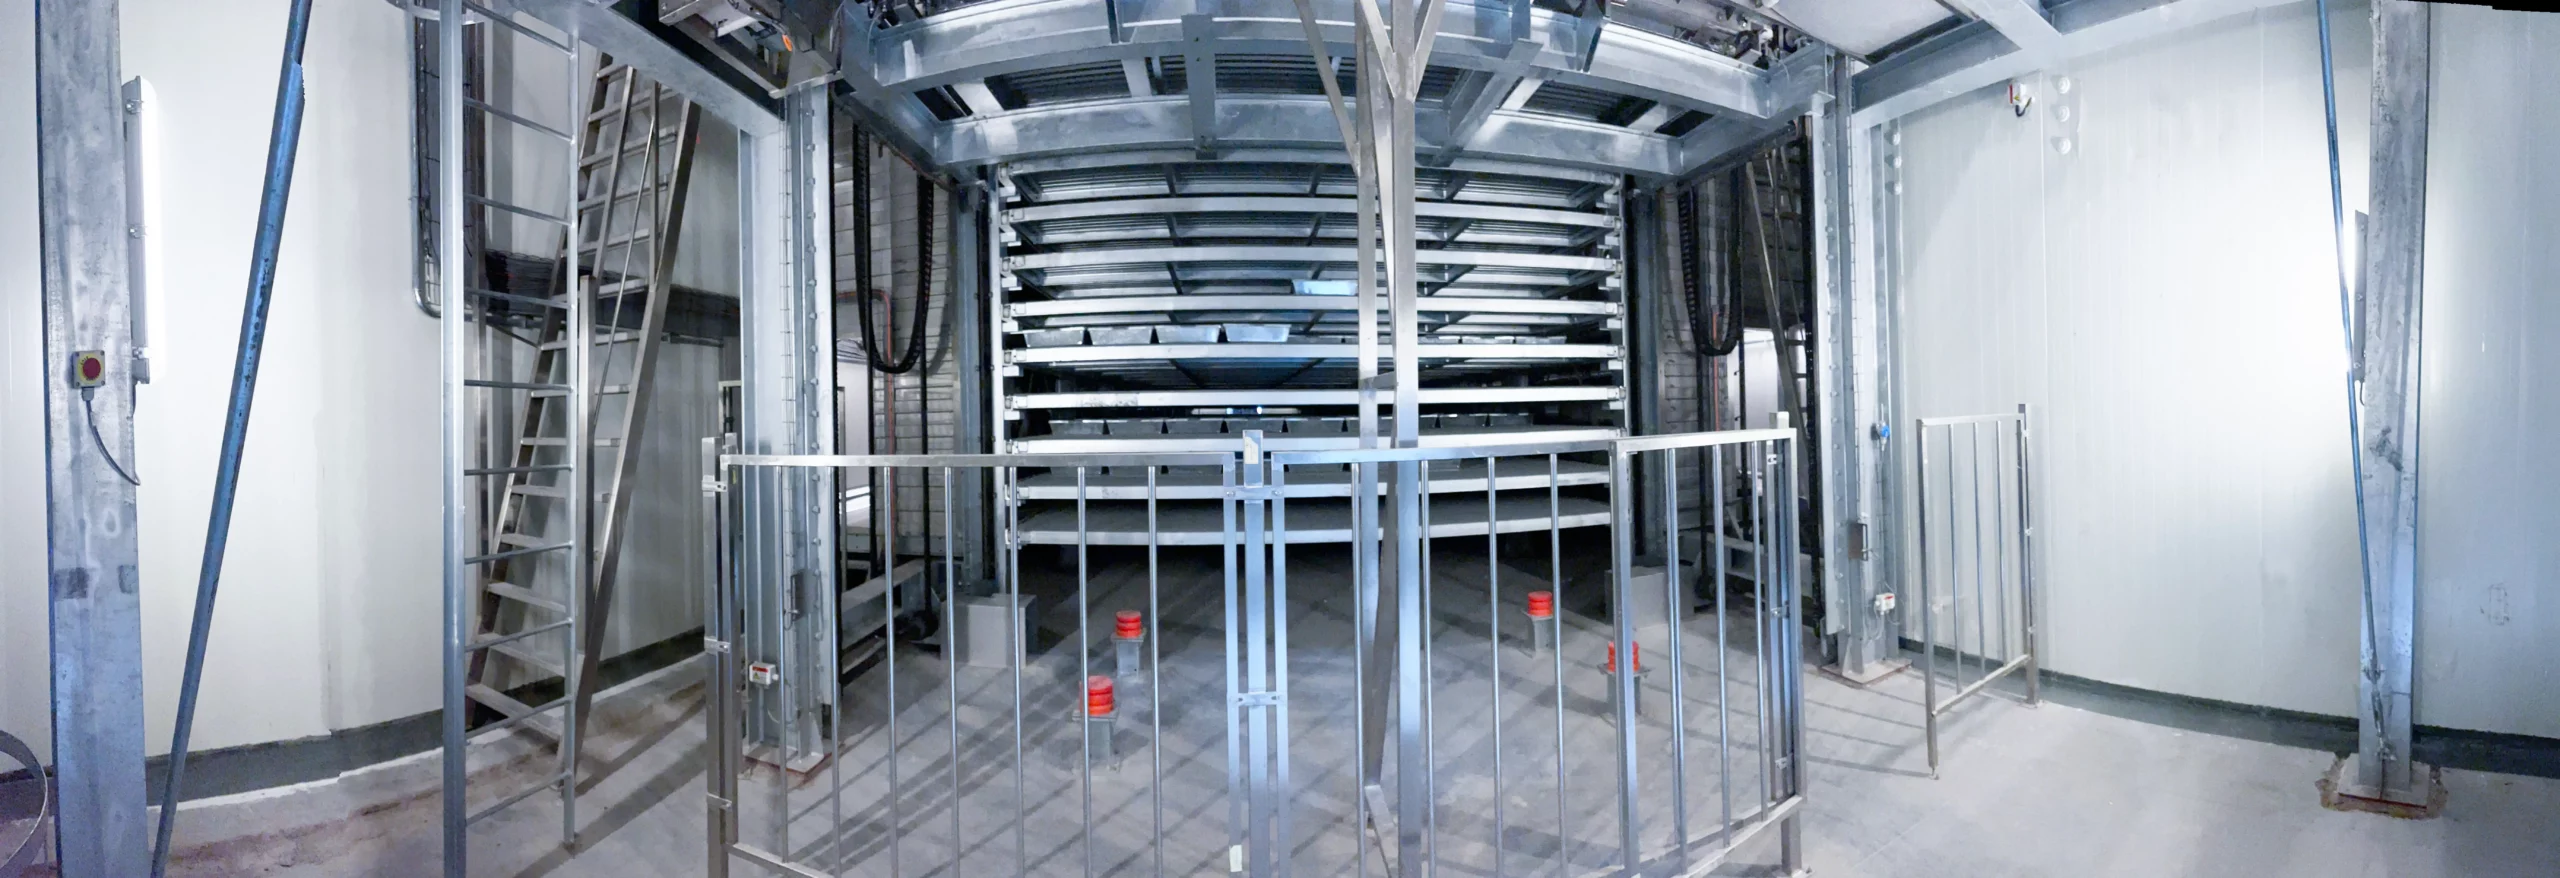
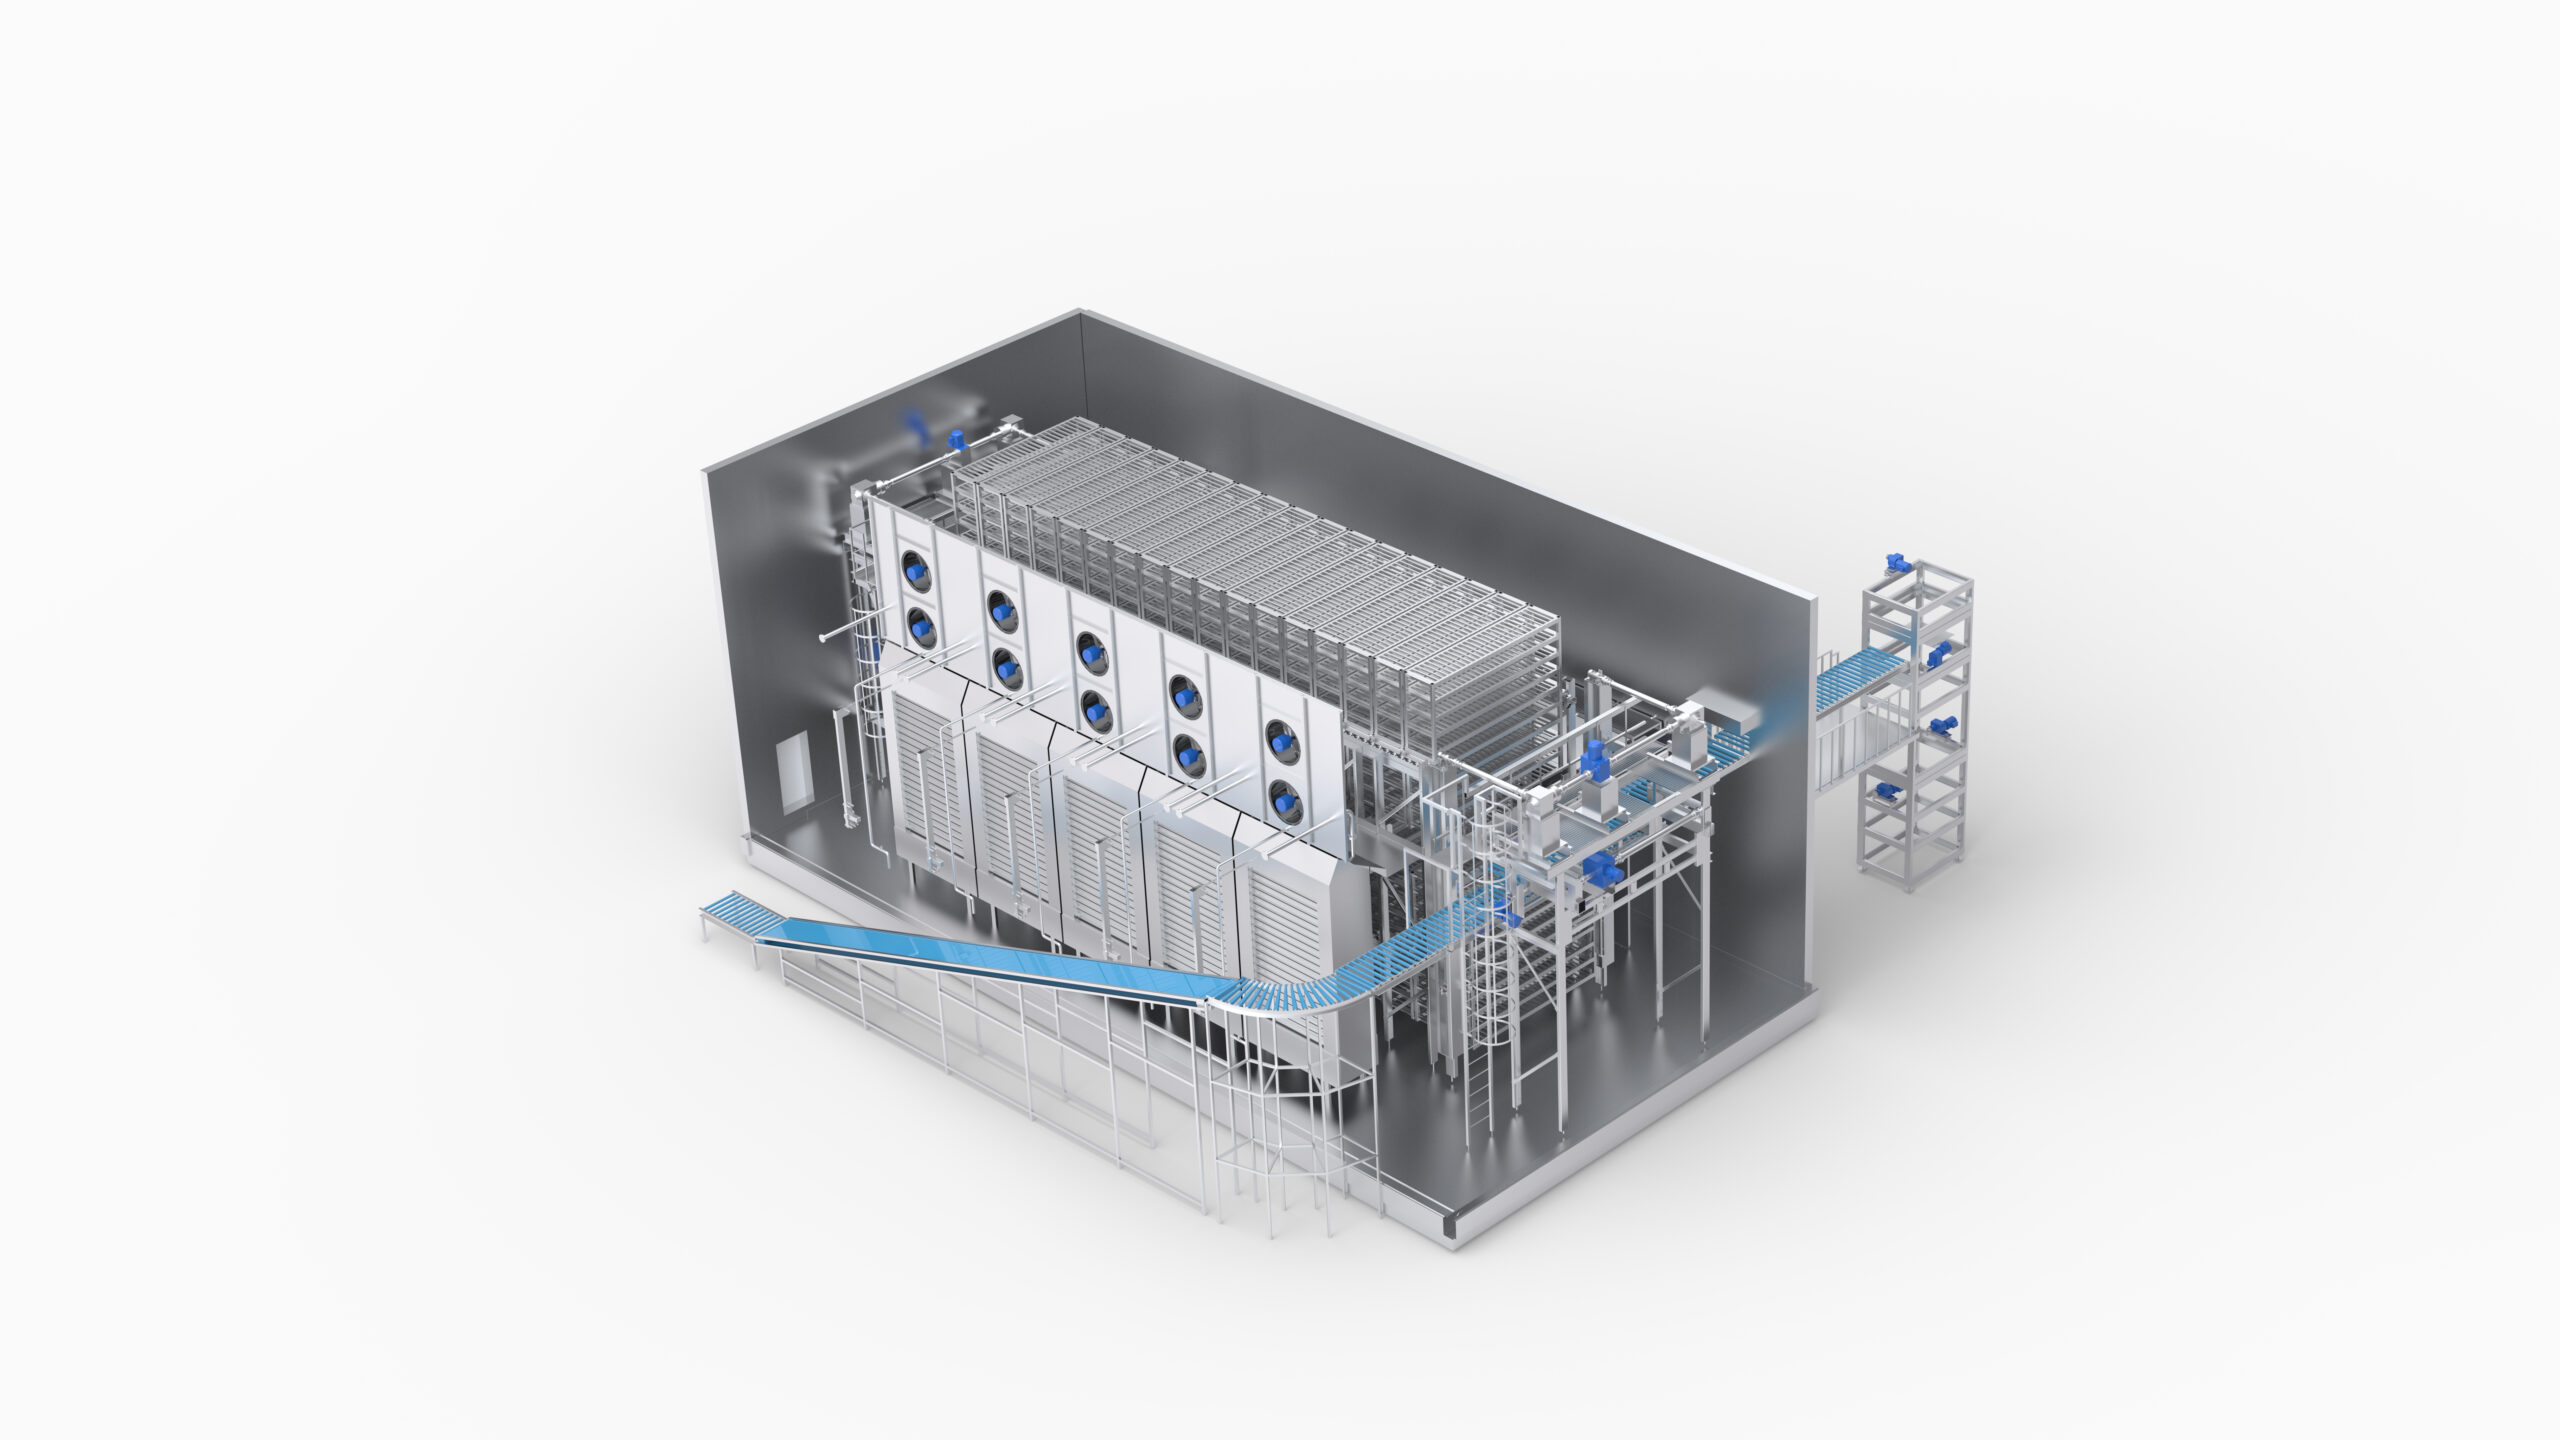
Fast horizontal airflow keeps air temperature and speed even across every tier, cutting freeze time and bringing every box to the same core temperature.
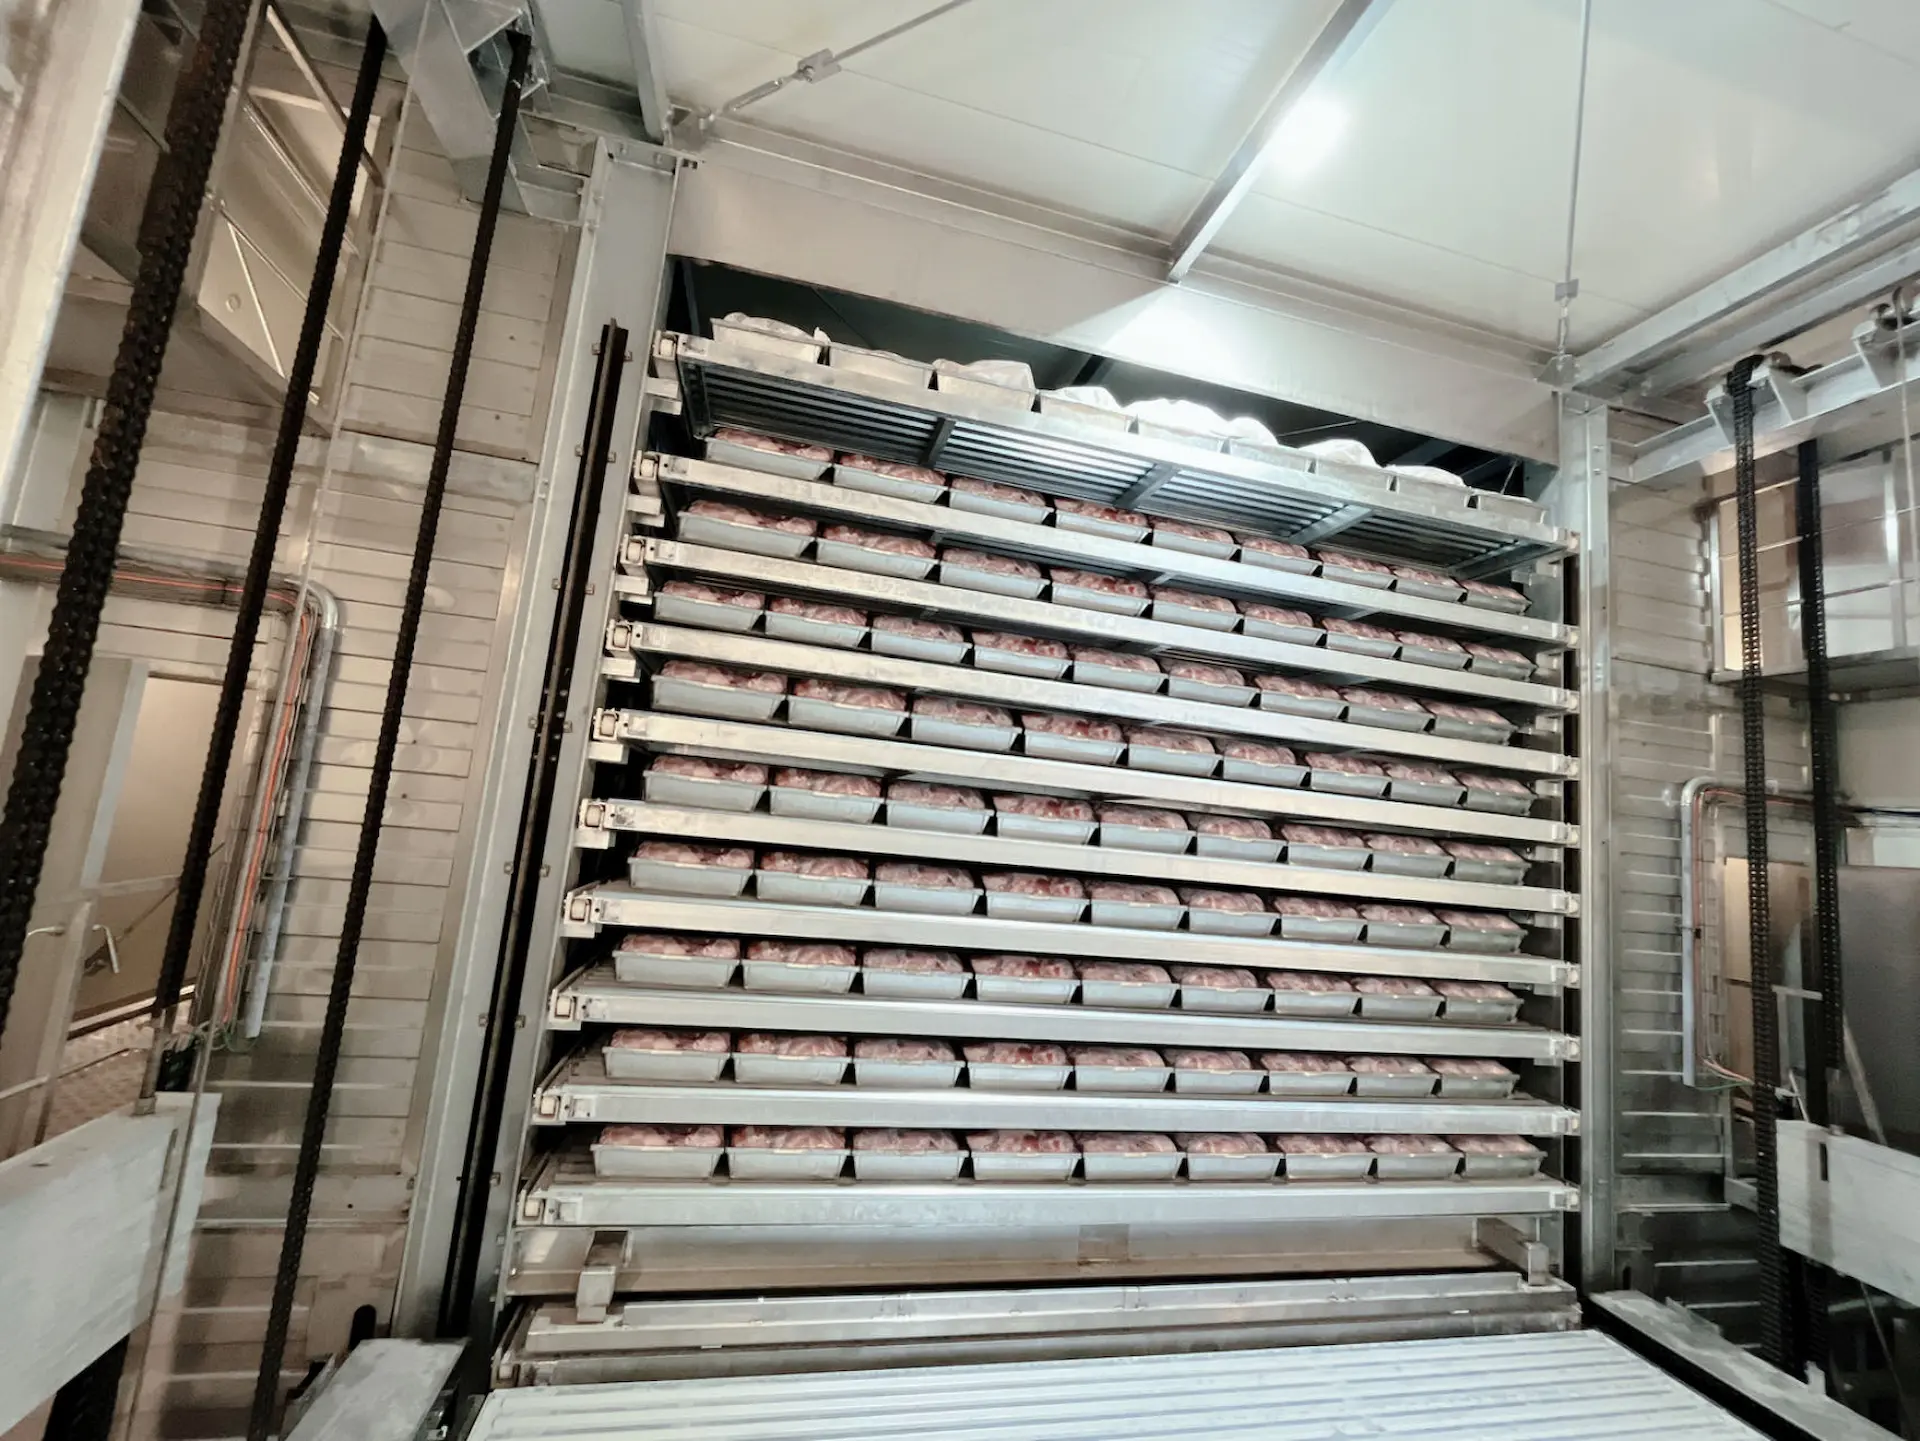
Automated infeed conveyors, vertical lifts, and pushers replace manual forklift work inside cold blast rooms.
Barcode scanners log the batch ID, entry time, tier number, and freeze time for every box, connecting directly with your warehouse software (WMS).
Separate conveyor tiers let you freeze boxes of different sizes and dwell times at the same time inside one enclosure.
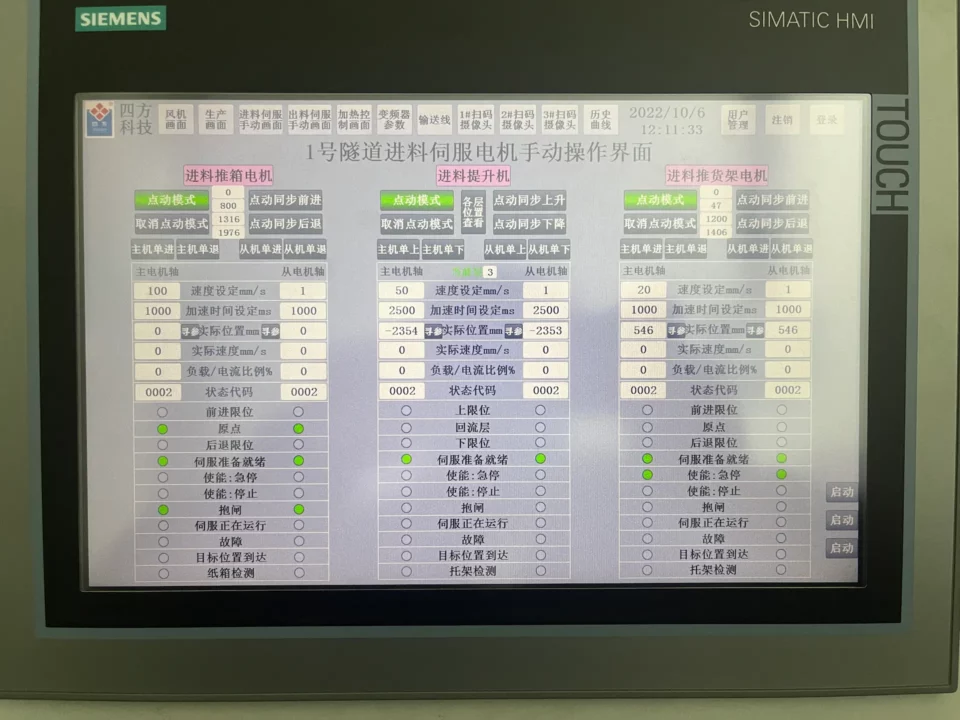
PLC and SCADA controls manage box loading, defrost timing, and remote diagnostics without operators entering the cold room.
Technical Specifications
Standard specifications are listed below. We size box holding capacity, tier count, dwell time, and conveyor links for your plant.
| Configuration | Multiple level conveyorized carton freezer: straight through or U-shape |
|---|---|
| Capacity | 2 to 15 tons/h (product and carton size dependent) |
| Carton sizes | 300×200×100 mm to 600×400×200 mm (standard); custom sizes accommodated |
| Conveyor levels | 2 to 6 levels for extended dwell time |
| Operating temperature | −35°C to −40°C (air); −40°C to −45°C (evaporating) |
| Refrigerant | NH₃ (Ammonia) / CO₂ (pump recirculated) |
| Evaporator | Industrial finned tube, stainless steel or aluminum, multiple bank |
| Defrost | Hot gas / Water, automated sequential defrost across multiple bank coils |
| Typical freeze time | 4 to 24 hours (carton size and product dependent) |
| Infeed / Outfeed | Automated conveyor with barcode scanning and palletizing interface |
| Control system | PLC with SCADA, WMS integration, batch traceability, automated reporting |
| Typical lead time | 18 to 24 weeks |
| Design life | 20+ years (structure); 15+ years (refrigeration); 8 to 12 years (conveyors) |
Design Details
Open each section below to see how key parts of the freezer work.
Carton freezers provide distinct operational advantages for boxed products:
Automated material handling coordinates carton flow from packing to palletizing:
Freezing time for cartoned product is governed by:
A standard 25 kg meat carton entering at +5°C typically reaches a −18°C core temperature in 10 to 16 hours at −38°C air temperature.
Carton freezers are engineered for high continuous thermal duties:
The carton freezer forms an automated bridge between packaging halls and cold storage warehouses:
Freezes 15 to 30 kg master cartons of boxed beef, pork, and poultry cuts to −18°C core temperature with flat, stackable box geometry.
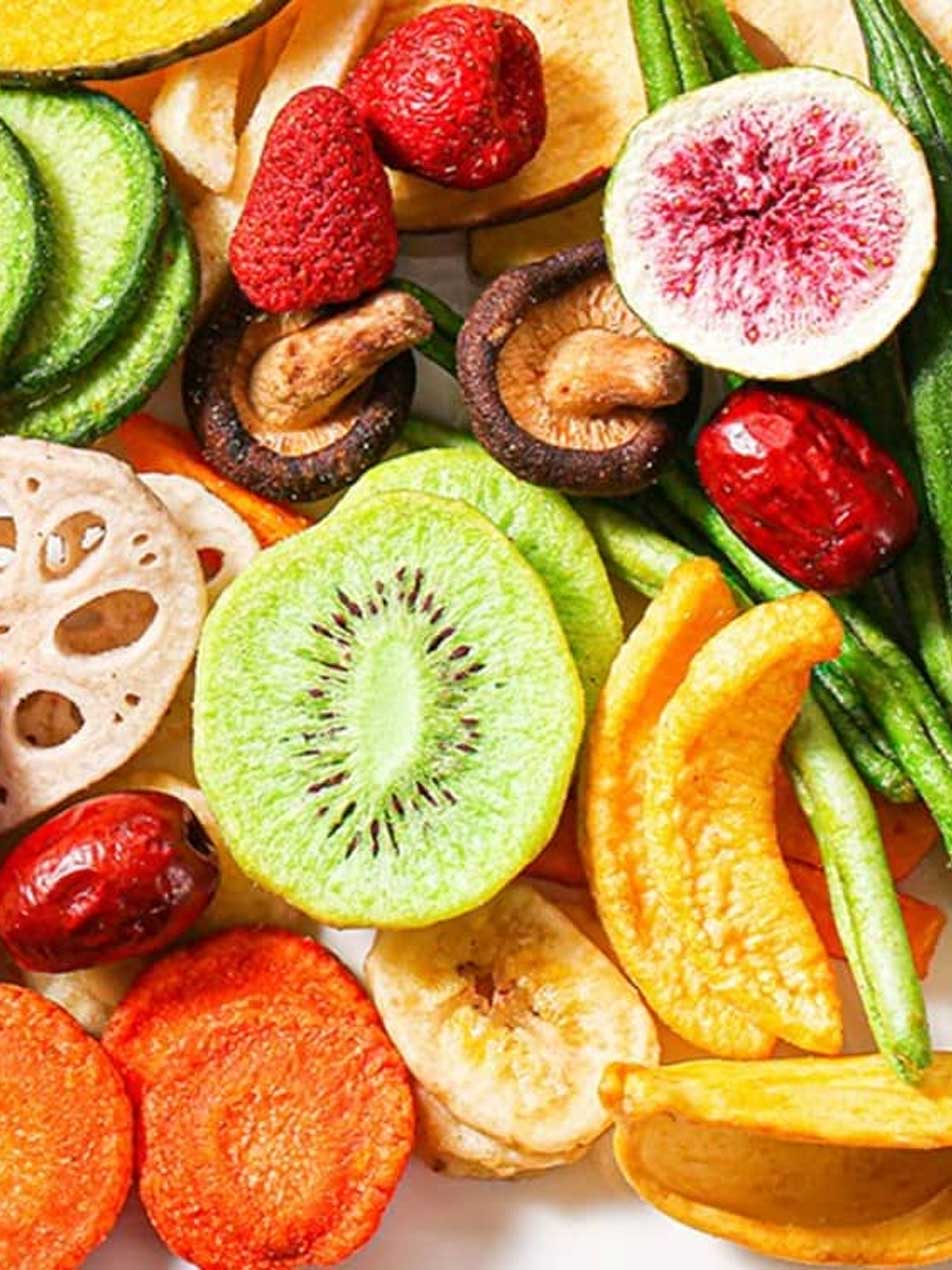
Chills and freezes boxed butter, cheese blocks, dairy ingredients, and bulk fruit cartons on variable retention multiple tier conveyors.
Case Studies
Proven installations running in food plants around the world.
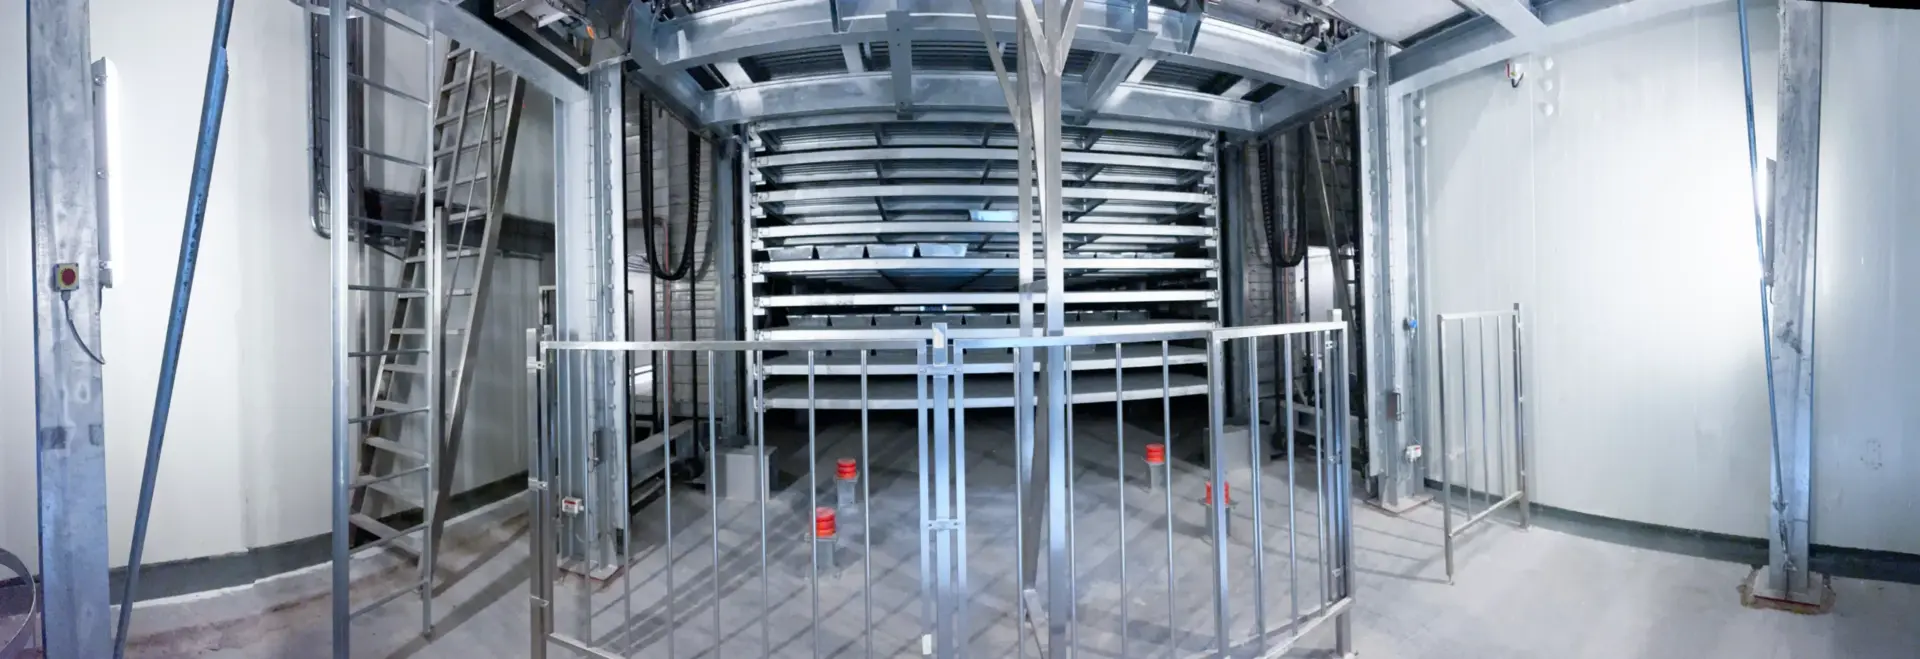
A multiple level automated carton tunnel freezer with conveyorized loading and discharge installed for boxed
No. Boxes ride flat on dedicated carriers with smooth pusher transfers and even airflow, preventing box crushing, bulging, or wet cardboard.
Yes. Our carton freezers connect directly with case packers, barcode scanners, checkweighers, robotic palletizers, and automated cold storage (AS/RS).
Square holds ISO 9001, ISO 45001, CE, PED, ASME (U and U2 stamps), EAC, CSA, CRN, and CNAS laboratory accreditation, supported by 300+ patents, 300+ R&D engineers, and 300+ installation and service engineers.
We customize tunnel length, tier count, airflow layout, loading height, cooling circuit, defrost, and WMS links to match your box sizes and hourly output.
The PLC assigns different box sizes to separate tiers and tracks each row’s exact dwell time, discharging each SKU only when its core reaches target temperature.
Engineering Inquiry
Share your box dimensions and cooling load for a carton freezer quote.